ISO 13124 specifies a test method for determining the interfacial tensile and shear bond strength of ceramic-ceramic, ceramic-metal, and ceramic-glass joining at ambient temperature by compression tests on cross-bonded test pieces. in the country of the requester. The work for Standardization) non-governmental, of preparing International right to body is a worldwide be in represented r. The work Standardization) of preparing International is a worldwide federation of national standards committee organizations, coll b rates standardization. This document. Studs and ceramic ferrules for arc stud welding is classified in these ICS categories: This document specifies the following: dimensions, materials and mechanical properties. In downloading this file, parties accept therein the re ponsibility of not infringing Adobe's licensing policy.
[PDF Version]
The Ceramic Ferrule Market must manage logistics risks associated with fragile ceramic components. Fluctuating industrial demand cycles affect production planning. 29 million in 2024 and is projected to touch USD 995. Various materials, including ceramic. Ceramic Ferrule by Application (Fiber Optic Connector, Other Active Devices, Other Passive Devices), by Types (SC and FC Ceramic Ferrule, ST Ceramic Ferrule, LC Ceramic Ferrule, Others), by North America (United States, Canada, Mexico), by South America (Brazil, Argentina, Rest of South America). The global ceramic ferrule market was valued at USD 382 million in 2024. This growth represents a CAGR of 10.
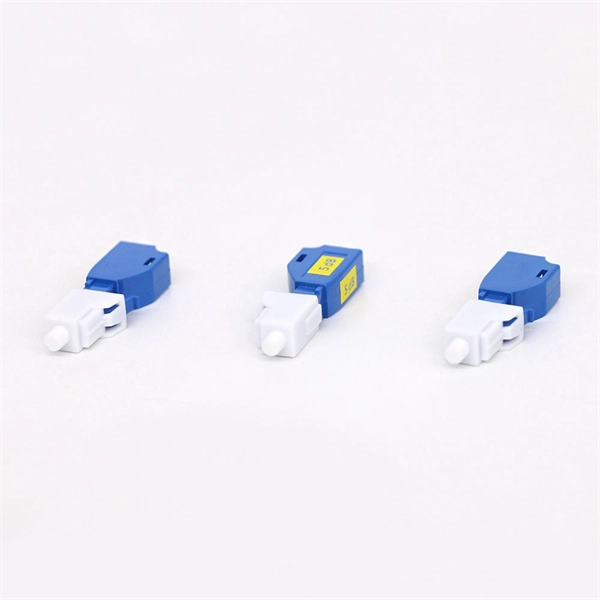
At its core, ceramic sintering is a high-temperature process that transforms a compacted powder into a solid, dense object. It achieves this not by melting the material, but by using heat to force the individual particles to fuse together, eliminating the empty spaces between them. The molded ferrules are placed in a furnace and heated to a temperature of around 1,500°C for several hours. This process is fundamental to the production of a wide range of ceramic products, from traditional pottery to advanced. With zirconia ceramic powder as a main material, an ethylene-vinyl acetate copolymer, an oleic acid, polymethacrylate, atactic polypropylene and paraffin are added in the mixing process, and thus the prepared zirconia ceramic ferrule is good in abrasive resistance, strong in ageing resistance. Ceramic ferrules are precision-engineered, cylindrical components manufactured from high-quality alumina, zirconia, or other advanced ceramic compositions.
[PDF Version]
An optical circulator is a three- or four-port designed such that entering any port exits from the next. This means that if light enters port 1 it is emitted from port 2, but if some of the emitted light is reflected back to the circulator, it does not come out of port 1 but instead exits from port 3. This is analogous to the operation of an electronic. Fiber-optic circulators are used to separate optical signals.
The intrinsic properties of most ceramics virtually rules out all methods of fusion welding. However, solid state techniques, adhesive bonding and brazing all remain as possible means of providing strong, sound joints between ceramics and metals. Joining ceramics to other materials, also known as ceramic-metal or ceramic-polymer joining, has been an area of extensive research and innovation. Engineers and scientists have been exploring various techniques to effectively bond ceramics, which are known for their high temperature resistance and. This step-by-step guide will walk you through the intricate process, covering everything from material selection to surface preparation and the application of filler metals. These assemblies are critical in industries where. To obtain the optimum performance from specific components, it is often necessary to join ceramic parts to other materials particularly metals.
[PDF Version]
Stainless steel tube OPGW: stainless steel tube is hermetically sealed by seamless welding. This tube provides complete protection to the fibers from longitudinal and lateral water/moisture ingress. The special production line of OPGW is equipped with high precision tension control multifiber payoff station, its. This fiber optic training course is designed for those who specify, design, install, construct or maintain aerial Optical Power Ground wire systems in investor-owned, Electric Power Utilities, REAs, Co-operatives, and municipal power networks. Students will learn about the latest construction. ation on high voltage overhead power lines. Furthermore this specification contains information concerning the quality assurance during manufacturing, the final accepta ce tests. — Limits apply to each fiber (vs. bare fiber specs) — Measured in dB/km at 1310 and 1550, plus 1625 nm is good to know What about other fiber types? — Multimode fiber is available for special applications: 62.
[PDF Version]
26 mm 2 (10 AWG) ground wire must be used, and in all other markets a 6 mm 2 must be used. Applying and maintaining proper grounding methods within the welding area is important to promote electrical safety in the workplace. Associated processes such as plasma cutting will also benefit from proper grounding. Each DISTRIBUTION BOX and controller must be grounded. When lightning strikes or a rogue voltage surge decides to crash the party, proper grounding steps in like a seasoned bouncer, redirecting danger away from. For example, for High And Low Voltage Distribution Cabinets, the distribution box needs to be grounded regardless of size. The grounding "bus" (grounding bus, PE bus) in the box is directly connected to the power ground wire or grounding system; 2. The supplier shall submit Type Test Repor of the Isolator for approval of Employer before commencement of supply. The Switch disconnector to e provided in the Distribution Box will be as per Emplo e as per IS:13411 (amended. There are a variety of different types of grounding that you may encounter while you are welding.
[PDF Version]
HSN Code 8544 refers to "Insulated 'incl. coaxial cable' and other insulated electric conductors, whether or not fitted with connectors; optical fibre cables, made up of individually sheathed fibres, whether or not assembled with electric. Find HSN Code or ITC HS Code and their GST Rates for your product with our HSN Code Search Tool. Search by either product name or HSN Code. enamelled or anodised' wire, cable 'incl. Welding cables are vital components in any welding operation, designed to withstand harsh environments and transmit high currents safely. For businesses dealing with these essential electrical conductors in India, correctly identifying their HSN (Harmonised System of Nomenclature) code is crucial. This code helps businesses identify Optical Fibre Cables | Other correctly for billing, taxation, and trade.
[PDF Version]
A fiber welding head is an innovative device used in optics and telecommunication. Engineered for harsh production welding applications with a fiber-coupled laser, FiberWELD ® is a robust head with simplified plumbing of coolant and gases. Per the end user's processing requirements. Get consistently superior welds with this ultra-reliable and highly modular processing head, compatible with any high-power, fiber-coupled laser up to 20 kW. Basic industrial modular optics (BIMO) are a versatile processing head system which can be configured in numerous ways to reliably perform. Designed to complement the industry's broadest range of industrial fiber lasers, IPG laser welding heads offer optimal performance across a variety of welding applications. has dedicated a decade to in-depth research in four core technology ecosystems: laser head welding and cutting hardware, optical lenses, system software, and welding robots. Since 2006, Shenzhen Worthing Technology Co.
[PDF Version]
Place the joint plate centrally on the joint area of the cable trays. To avoid damage to cables, edge protection strip is attached at cut edges of cable trays, if no joint plates or bottom end plates are to be mounted. Cut the edge protection strip to size. The following pages address the 2014 National Electrical Code® requirements for cable tray systems as well as design. Cable tray welding is essential for ensuring the structural stability of cable tray systems in industrial and commercial wiring setups. Cable tray welding enhances the durability of. Our tray features our Safe-T-Edge design that involves "T" welding the lateral wires to the bottom edge of the top wires and carries a patent for optimized wire diameters for maximized working load.
[PDF Version]Contact us for competitive quotes on any of our fiber optic products
Get a Quote